Machining Centers
Choose between vertical, horizontal, and gantry machining centers using the complete part and fixture envelope, required access, table load, and operation sequence.
Send Your Part Drawing
VMC, HMC, and GMB Series
The catalog lists compact through larger vertical machining centers, horizontal models, and gantry machines for larger setups.

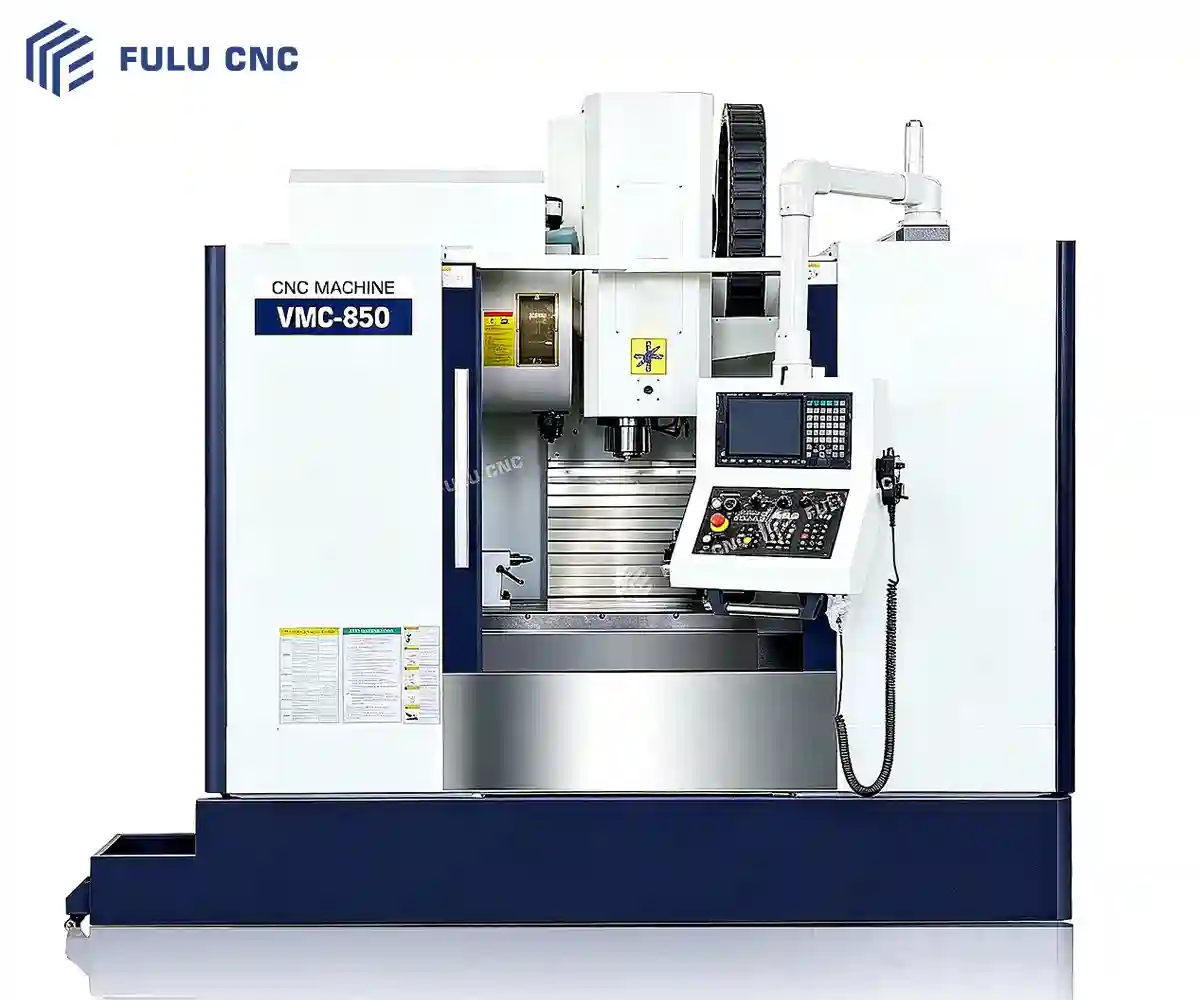
VMC vertical machining centers
VMC640, VMC650, VMC850, VMC855, VMC1160, VMC1265, VMC1370, VMC1580, and VMC1890. Compare X/Y/Z travel, spindle-to-table clearance, table size, and load.

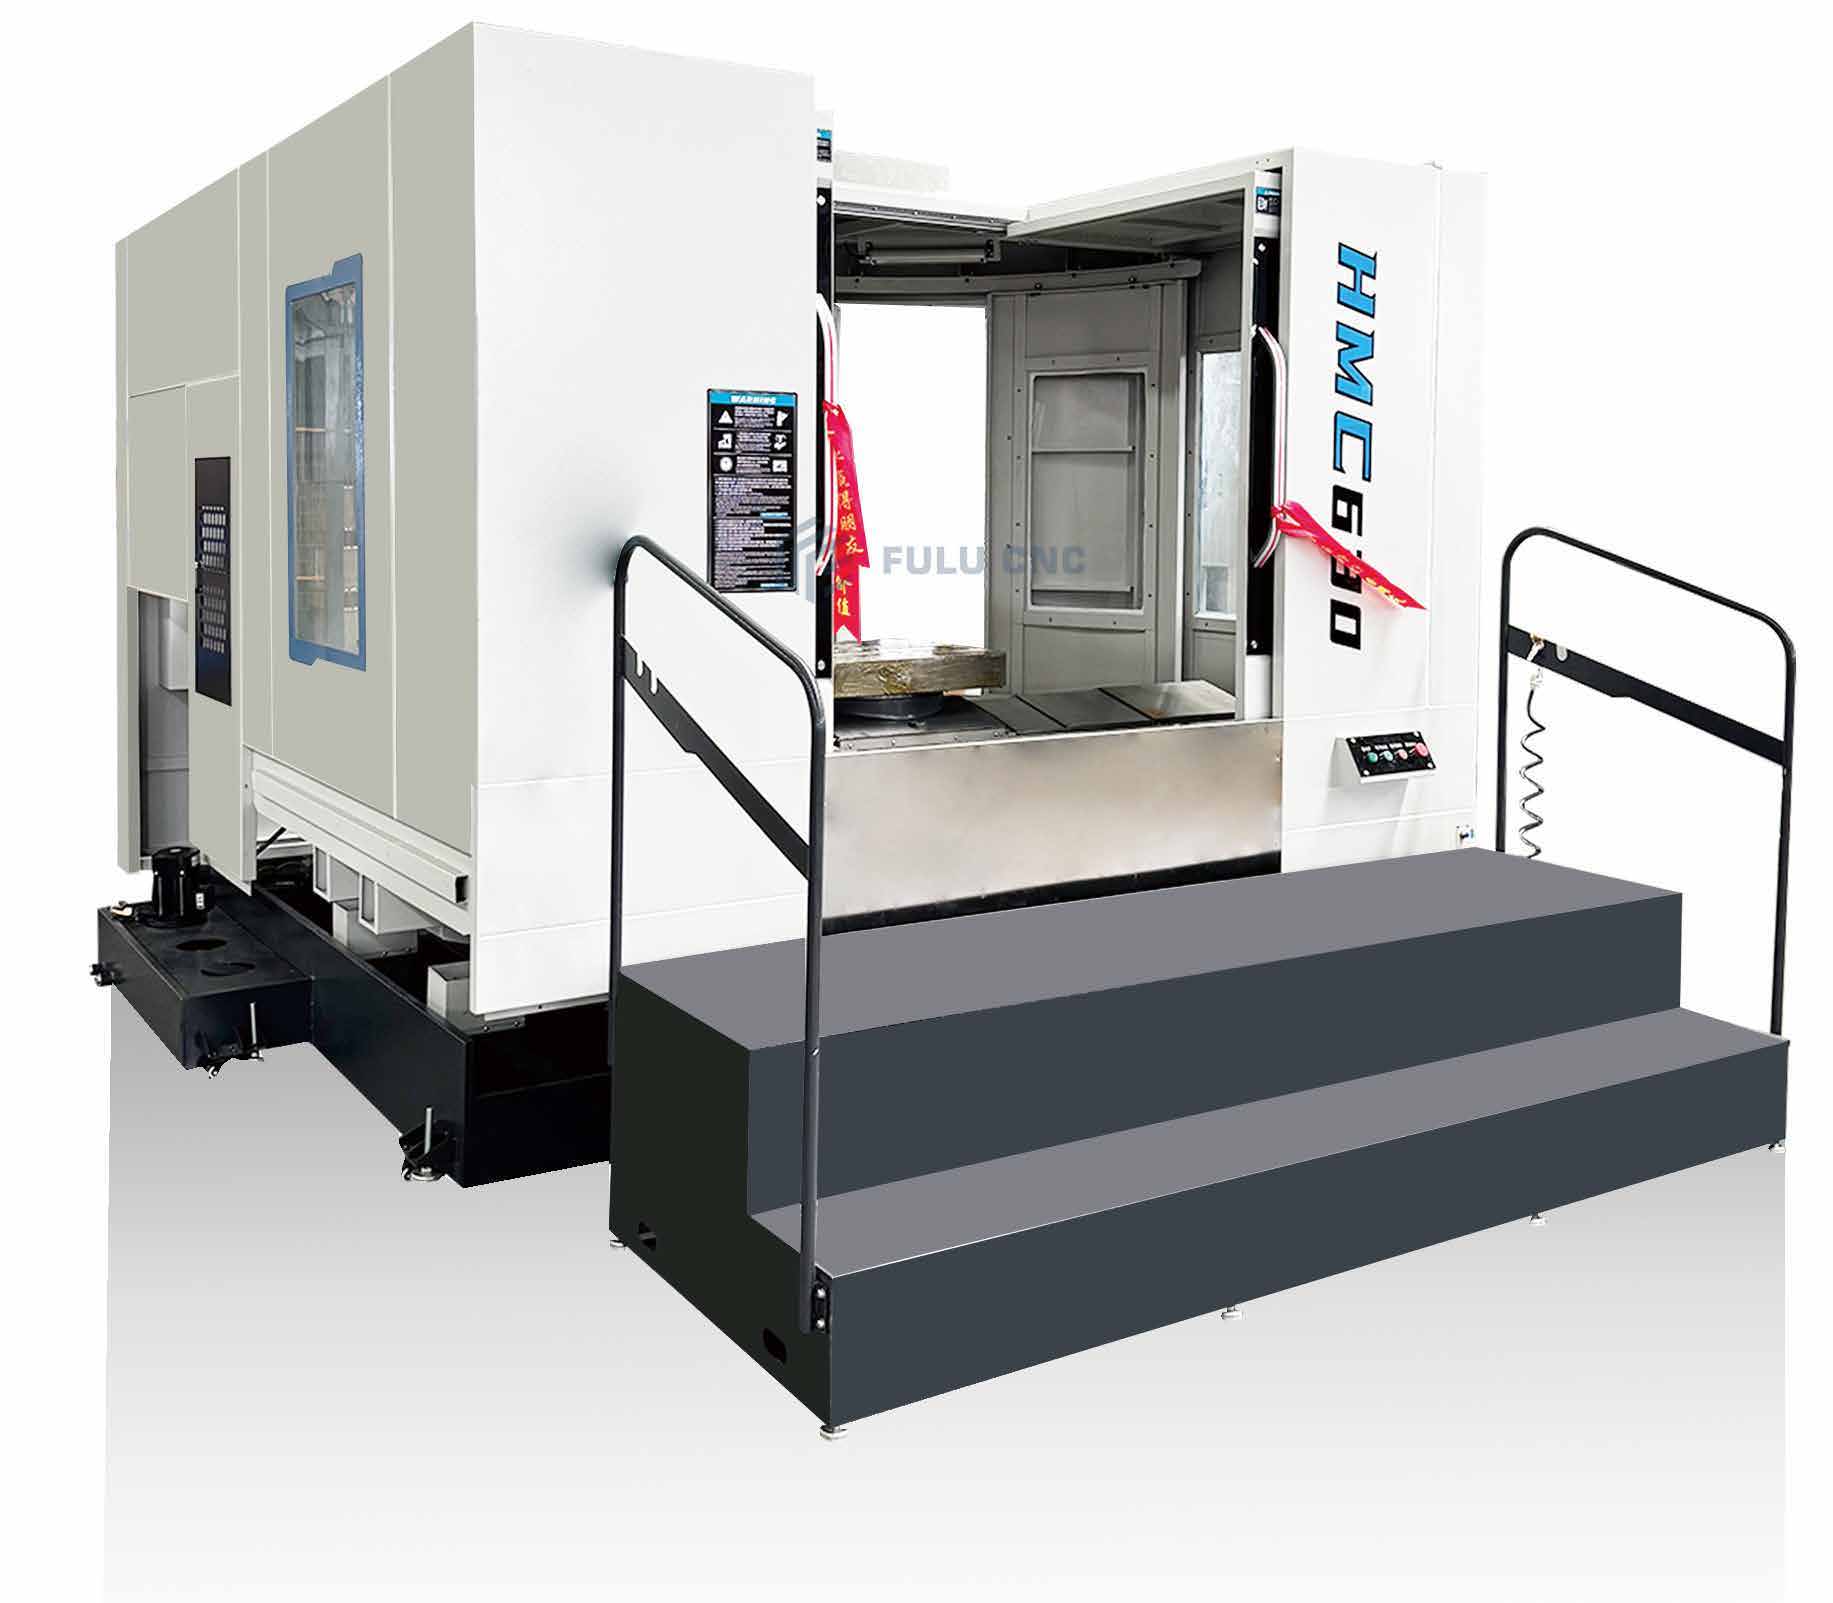
HMC horizontal machining centers
HMC500, HMC630, HMC800, HMC1000, HMC1380, and HMC1580 are listed. Confirm pallet and rotary configuration for the selected machine.

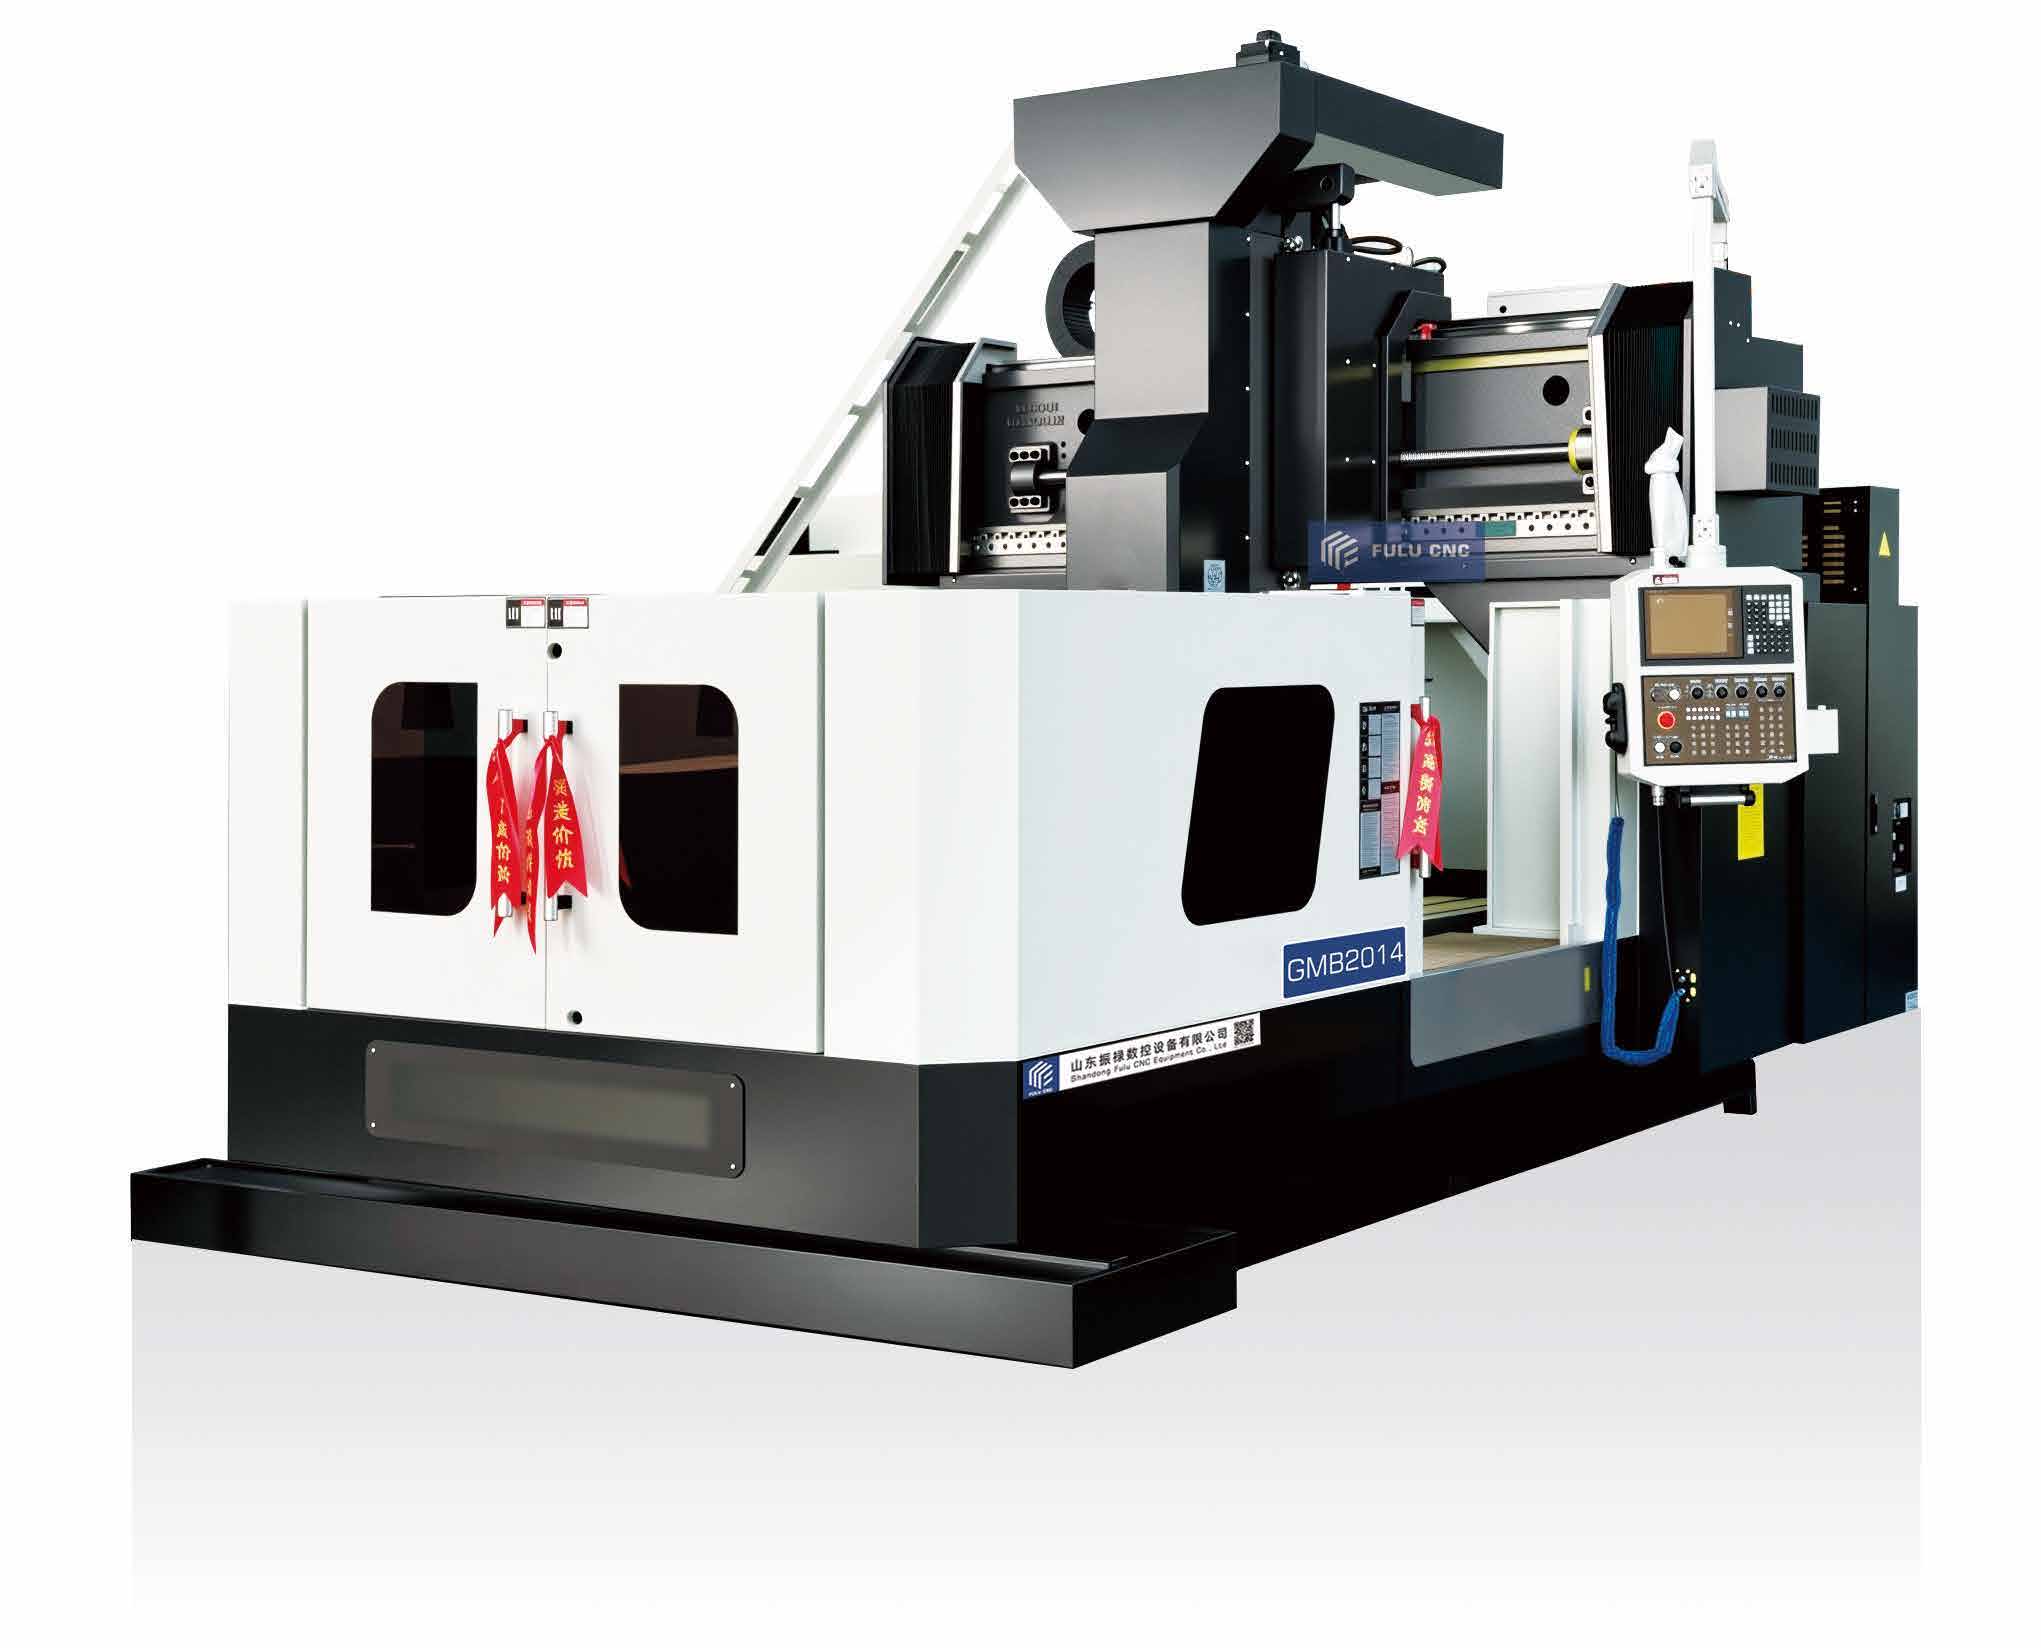
GMB gantry machining centers
GMB2014, GMB2016, GMB2518, GMB2720, GMB3220, GMB4220, and GMB6025 are listed. Review travel, load, lifting, and site requirements.
Choose Around Access and Setup
The right machine depends on the complete workpiece plus fixture, not the nominal size of the bare part.
A VMC is a starting point when the operation plan is mainly accessible from above. Check fixture height, tool length, spindle-to-table clearance, X/Y/Z travel, and table load.
Evaluate an HMC when the drawing and fixturing benefit from horizontal access or a selected rotary/pallet arrangement. The exact pallet and indexing equipment must be confirmed for the quoted model.
Evaluate a GMB gantry model against the loaded workpiece envelope, tool approach, lifting method, floor space, foundation, and utilities. Table size alone is insufficient.
Specify the required faces, angles, and toolpaths. Confirm rotary axes, controller functions, interference envelope, and whether the equipment is standard or optional.
What Changes Between VMC, HMC, and GMB?
| Series | Selection trigger | Verify before quoting |
|---|---|---|
| VMC | Vertical tool access fits the fixture and planned operations. | Travel, spindle-to-table range, table/load, ATC, spindle, and optional axes. |
| HMC | Horizontal access or a specified pallet/indexing workflow is needed. | Pallet size and load, rotation, workpiece sweep, tool reach, and configuration. |
| GMB | The loaded setup exceeds the useful envelope of smaller architectures. | X/Y/Z access, table/load, head clearance, lifting, foundation, and installed utilities. |
The manual lists VMC, HMC, and GMB model ranges; the selected machine still needs a model-level specification and option check.
Check the Complete Setup Envelope
Travels and clearance
Include fixture height, tool length, spindle-to-table space, and side access.
Table and load
Add the workpiece and fixture mass, including offset loading and clamping space.
Process and access
List all faces to machine and decide whether vertical, horizontal, or gantry access fits the process.
Tooling and acceptance
Confirm spindle, tool system, coolant, optional axes, and the agreed inspection plan.
Travel, Table Size, and Load Are Separate Limits
Axis movement does not equal the largest part that can be machined. Include the vise or fixture, clamps, cutter diameter, tool approach, and clearance at each end of the stroke.
Add the workpiece, fixture, and clamping mass. Check how the load is distributed and whether it remains within the quoted table or pallet limits throughout the program.
Check both the shortest and longest tool/setup combination. A tall fixture may fit on the table but leave too little clearance for the toolholder or operation.
Do not infer included rotary axes or pallet hardware from the HMC family name. Ask for the specific equipment list and the resulting usable work envelope.
Two Reference Models, Different Scales
The table compares two exact model entries from the catalog. It does not define the full family range.
| Model | X / Y / Z travel (mm) | Table (mm) | Maximum table load (kg) |
|---|---|---|---|
| VMC850 | 800 / 500 / 500 | 1,000 × 500 | 500 |
| GMB2014 | 2,000 / 1,500 / 800 | 2,100 × 1,200 | 4,500 |
Check clearance, spindle configuration, fixtures, and machine-specific options in the current quotation.
Review the VMC850 in Detail
The VMC850 model page includes its specific working envelope, configuration notes, and selection guidance.
Machining Center FAQ
Which measurement comes first when selecting a VMC?
Start with the workpiece and fixture envelope, then verify X/Y/Z travel, spindle-to-table distance, table size, and maximum load.
Does an HMC model name confirm the pallet system?
No. Ask for the selected pallet dimensions, rotary arrangement, clearances, and equipment list.
Can a gantry machine be chosen by table size alone?
No. Include part and fixture weight, X/Y/Z access, head and tool clearance, loading method, foundation, and utilities.
Are rotary axes standard on these models?
Do not assume so. Specify the required indexing or simultaneous machining and confirm the complete axis, controller, and integration scope.
Does the X/Y/Z travel prove that my fixture fits?
No. Check the complete clamped setup, toolholders, spindle-to-table range, table load, and clearance through every operation.
What should be included when comparing VMC850 with a gantry model?
Compare the actual workpiece plus fixture envelope, all machining faces, travel, table load, spindle/tool access, loading method, and installation requirements. The catalog values belong to individual models.
Review Your Milling Process
Send the drawing, material, workpiece and fixture dimensions and mass, faces and operations, tolerance and finish requirements, batch volume, tool and spindle needs, destination, and electrical requirements.
Send Your Part Drawing